Overview of CNC Connection Manuals
Connection manuals are essential for CNC setup‚ offering wiring diagrams‚ configuration steps‚ and safety notes. They guide operators through proper linking of components‚ ensuring reliable communication and optimal machine performance. They also include troubleshooting.
Purpose and Scope
The purpose of a CNC connection manual is to serve as a definitive guide for establishing reliable electrical and signal links between all components of a CNC system. It defines the scope of the documentation‚ covering every aspect of wiring‚ signal definition‚ configuration‚ and safety compliance required to connect a machine to its controller‚ drives‚ and peripheral devices. The manual is intended for operators‚ maintenance technicians‚ and system integrators‚ providing step‑by‑step instructions that ensure each cable‚ connector‚ and signal path is installed according to the manufacturer’s specifications and industry best practices. By detailing cable routing‚ connector types‚ voltage levels‚ and signal assignments‚ the manual enables accurate troubleshooting‚ efficient maintenance‚ and seamless upgrades while safeguarding against electrical hazards and ensuring system integrity. It also serves as a reference for future modifications‚ allowing teams to document changes and maintain traceability throughout the machine’s lifecycle.
- Provides a single source of truth for all wiring and signal connections.
- Ensures compliance with safety standards and reduces risk of electrical faults.
- Facilitates rapid troubleshooting and reduces downtime during maintenance.
- Supports future upgrades and system expansions with clear documentation.
- Improves communication between operators‚ technicians‚ and engineers.
By following the manual‚ teams can confidently install‚ verify‚ and maintain CNC connections‚ ensuring optimal performance.
Key Components Covered
Connection manuals enumerate the essential hardware and software elements that must be linked for a CNC system to operate correctly. The documentation lists every cable type‚ terminal block‚ and connector style required to interconnect the controller‚ servo drives‚ spindle‚ coolant system‚ and safety interlocks. It specifies the exact voltage‚ current‚ and impedance values for power supplies‚ ensuring that each module receives the proper electrical environment. Signal lines—digital‚ analog‚ and fieldbus—are identified with their pin assignments‚ polarity‚ and shielding requirements‚ allowing technicians to verify continuity and eliminate noise. The manual also catalogs the firmware and configuration parameters that must be programmed into the controller‚ such as motion profiles‚ axis limits‚ and safety overrides. Finally‚ it provides a comprehensive list of safety definitions and best‑practice guidelines‚ covering emergency stop circuits‚ lockout/tagout procedures‚ and grounding schemes. By covering these components in detail‚ the manual guarantees that every link in the chain is correctly installed‚ tested‚ and documented.
- Wiring diagrams illustrate cable routes and pinouts.
- Configuration tables map controller settings to hardware.
- Safety interlocks ensure operator protection.
- Documentation standards aid future maintenance.
These manuals are references that streamline installation‚ reduce errors‚ and support compliance with industry safety standards.
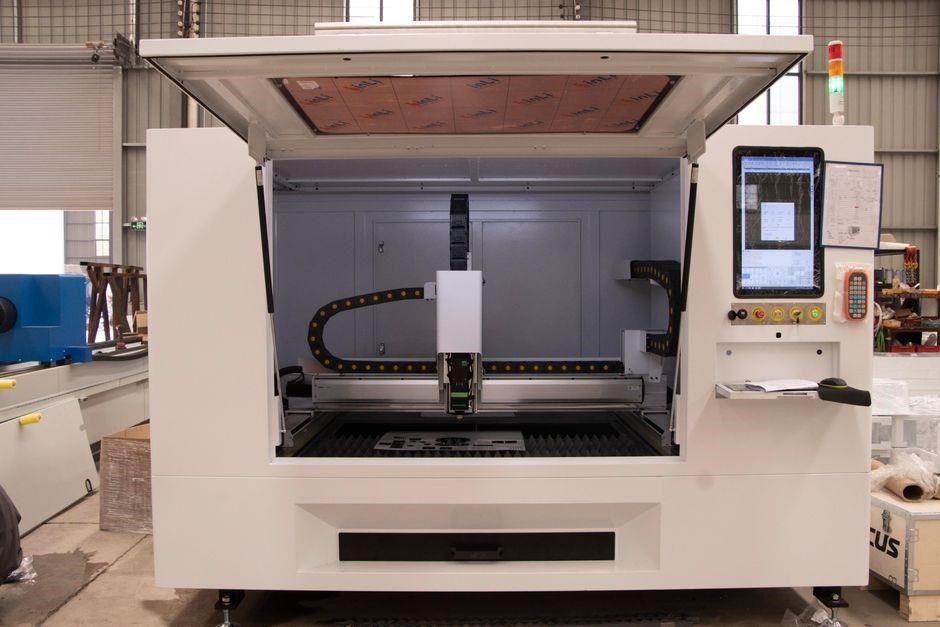
Fanuc CNC Connection Manuals
These manuals provide wiring diagrams and configuration steps for Fanuc CNC systems‚ ensuring correct links between controller‚ drives‚ and safety devices. They aid operators in installation and troubleshooting efficiently fast!.
Wiring Diagrams
Fanuc CNC connection manuals contain detailed wiring diagrams that illustrate the electrical pathways between the CNC controller‚ servo drives‚ spindle motors‚ safety interlocks‚ and operator interfaces. Each diagram specifies terminal numbers‚ cable types‚ and signal colors‚ enabling technicians to trace connections accurately. The manuals also provide step‑by‑step assembly instructions‚ ensuring that power feeds‚ grounding‚ and signal integrity are maintained. By following these diagrams‚ users can avoid common wiring errors such as reversed polarity‚ incorrect grounding‚ or mismatched cable gauges‚ which can lead to equipment damage or unsafe operating conditions. Additionally‚ the diagrams include reference numbers for replacement parts and highlight critical safety points‚ such as emergency stop wiring and lock‑out tags. The visual layout of the diagrams supports quick verification during installation and routine maintenance‚ reducing downtime and improving overall machine reliability.
In addition‚ the manuals provide color‑coded cable charts‚ terminal block diagrams‚ and recommended cable routing paths to minimize electromagnetic interference. They also list the permissible voltage ranges for each signal type and specify the required isolation distances between high‑current and low‑current circuits. The diagrams often include a troubleshooting matrix that correlates common fault codes with specific wiring faults‚ allowing operators to quickly identify and correct miswired connections.
Appendix
Configuration Procedures
Fanuc CNC connection manuals offer step‑by‑step configuration procedures that guide operators through setting up communication protocols‚ assigning IP addresses‚ and calibrating motion parameters. The manuals detail how to load firmware‚ configure safety interlocks‚ and map input/output channels to the controller’s internal logic. They emphasize the importance of verifying signal integrity and ensuring that all safety definitions are correctly implemented before commissioning. For the S625 CNC interface‚ the guide provides explicit instructions on configuring signal timing‚ voltage levels‚ and grounding schemes to meet the specifications of conventional bending presses. The CNC Machine Tool Builders Guide supplements these steps by outlining model‑specific settings‚ describing the use of signal symbols‚ and defining safety parameters that must be met for each machine type. By following these procedures‚ operators can achieve reliable‚ fault‑free operation and maintain compliance with industry safety standards. Additionally‚ the manuals instruct on setting up diagnostic tools and calibrating spindle speeds. They cover network configuration‚ detailing IP addressing and firewall rules to ensure secure communication. Operators are guided through routine checks to confirm that all safety interlocks emergency stop circuits are functional before production.!
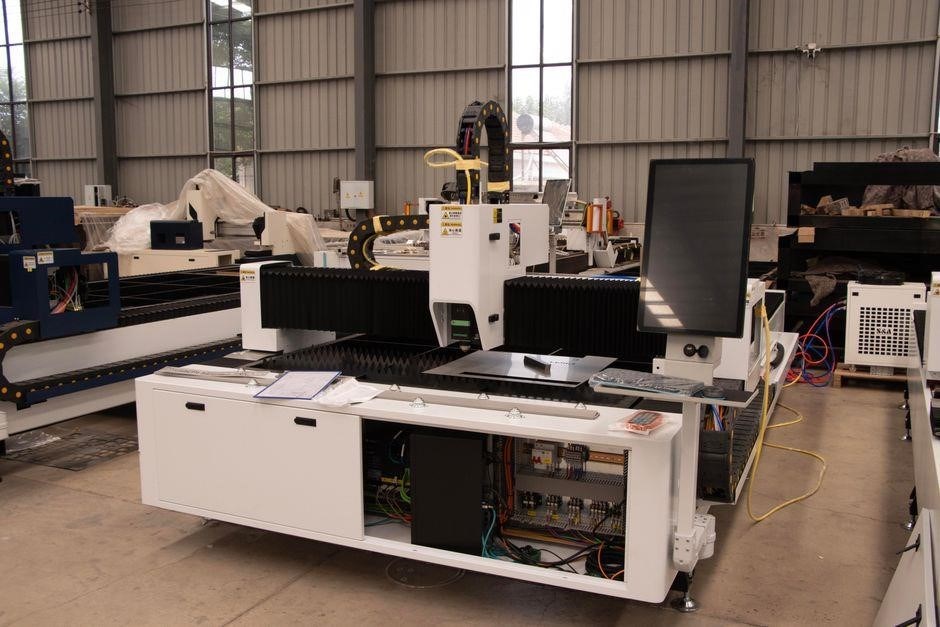
S625 CNC Interface and Connection Guide
The S625 CNC Interface and Connection Guide details power supply requirements‚ connector types‚ and signal specifications for conventional bending presses. It includes wiring diagrams‚ installation steps‚ and safety definitions to ensure proper setup and compliance.
Power Supply Requirements
The S625 CNC Interface requires a dedicated 480 V‚ 3‑phase‚ 60 Hz power supply with a minimum 10 kW rating to support spindle operation. The supply must provide isolated 24 VDC for control logic‚ with a ripple tolerance of less than 50 mV and a noise level below 5 mV RMS. Grounding must follow IEC 60204‑1 standard‚ using a single‑point earth connection to prevent differential‑phase voltages. The interface’s power module includes a 3‑phase 4‑pole brushless rectifier that converts the incoming AC to regulated DC‚ feeding the spindle motor controller and the I/O logic. Surge protection is mandatory; a surge‑voltage‑suppression (SVS) device rated at 10 kV must be installed on each phase. The power cable must be a minimum 4‑AWG copper‚ with a temperature rating of 90 °C and a minimum insulation class of 450 V. Cable routing should avoid proximity to high‑frequency signal lines to reduce electromagnetic interference. The interface’s power connector is a 3‑pin‚ 5‑amp‚ 250 V IEC‑60320‑D type‚ designed for quick‑disconnect. All power connections must be tightened to a torque of 12 Nm to ensure mechanical stability. Finally‚ the power supply must be certified by a recognized testing laboratory (e.g.‚ UL‚ CSA‚ or IEC) and include a built‑in fault‑current limiter that trips at 30 A to protect the spindle and control electronics from overload!
Electrical Connector Specifications
The S625 CNC interface utilizes a standardized 2‑pole‚ 4‑wire‚ 5‑amp‚ 250 V IEC‑60320‑D connector for power‚ and a 3‑pole‚ 4‑wire‚ 5‑amp‚ 250 V IEC‑60320‑D connector for ground. Signal connections employ a 16‑pin‚ 2‑row‚ 0.5‑inch pitch‚ 1‑inch wide‚ 4‑pole‚ 5‑amp‚ 250 V DIN rail mount connector‚ rated for 10 kW. The connector’s pins are gold‑plated to reduce corrosion and provide a contact resistance of <0.1 Ω. Cable insulation is 450 V‚ 90 °C rated‚ and the cable jacket is UL‑listed. The connector’s keying scheme matches the S625’s pinout: pins 1–4 carry 24 VDC signals‚ pins 5–8 carry 4‑wire 480 V AC‚ pins 9–12 carry 4‑wire 480 V AC for the spindle motor‚ and pins 13–16 carry 4‑wire 480 V AC for the I/O logic. The connector’s mounting flange is 1‑inch wide‚ 1‑inch high‚ and includes a 1‑inch key to prevent mis‑orientation. The connector’s locking mechanism is a 3‑pin‚ 5‑amp‚ 250 V latch that snaps into place‚ providing a secure connection even under vibration. The connector’s specifications are fully compliant with IEC 60204‑1 and ISO 13849‑1‚ ensuring safe operation in industrial environments. The connector’s strain relief absorbs up to 200 N of pull‚ and its 90° angled cable entry reduces bending stress. The mounting flange bolts with 4×10 mm screws for secure attachment. Documentation includes wiring diagram and quick‑start guide.
CNC Machine Tool Builders Guide
This guide details signal descriptions‚ symbols‚ and safety definitions for FANUC Series O and O Mate CNCs. It outlines applicable models‚ manual organization‚ and troubleshooting tips to ensure correct installation and operation.
Signal Descriptions and Symbols
The signal section of the CNC Machine Tool Builders Guide decodes every electrical line that powers a FANUC Series O or O Mate machine. Each line is identified by a unique code‚ a descriptive label‚ and a symbol that appears on the wiring diagram. For example‚ the spindle speed signal is marked SPD and represented by a circular arrow icon‚ while the feed rate uses FRT with a straight arrow. The guide also explains the polarity of each signal‚ the required voltage range‚ and the permissible current. It includes a table that lists all input and output signals‚ their functions‚ and the recommended cable type. In addition‚ the manual describes how to interpret the symbol set used for safety interlocks‚ emergency stops‚ and status indicators‚ ensuring that builders can correctly wire the machine and verify that all safety features are active. By following these signal descriptions and symbols‚ technicians can avoid miswiring‚ reduce downtime‚ and maintain compliance with industry safety standards. The document further details the use of digital inputs such as DI1–DI8 for limit switches‚ DO1–DO4 for spindle control‚ and analog outputs like AO1 for coolant flow. It explains the encoding of status bits in the machine’s status register‚ how to read them via the STATUS bus‚ and how to map them to the operator’s panel. The guide also provides troubleshooting tips for common signal faults‚ such as short circuits‚ open circuits‚ and incorrect voltage levels‚ and offers recommended diagnostic tools. Finally‚ it lists the standard symbols used across all FANUC manuals‚ including the universal “X” for unknown signals‚ the “!” for critical alarms‚ and the “✓” for confirmed connections.
For advanced users‚ the guide also covers the use of the IO-Link protocol‚ detailing how to integrate smart sensors and actuators‚ and explains the configuration of the PLC interface for extended automation. This ensures seamless integration with factory automation systems.
Safety Definitions and Practices
In the CNC Machine Tool Builders Guide‚ safety definitions set the terms used in the manual. “Emergency Stop” (E‑Stop) cuts power to the spindle and coolant‚ stopping motion immediately. “Interlock” disables the machine until a safety gate or light curtain is closed. “Safe‑Operating Zone” (S‑OZ) is the area where operators may enter without triggering an alarm. The guide requires all safety devices to be rated for the machine’s voltage and current‚ and to be tested after installation and routine maintenance. Lock‑out/tag‑out (LOTO) must be applied before any service work. The manual recommends color‑coded cables—red for power‚ yellow for signal‚ green for ground—to reduce wiring errors. Grounding all metal parts prevents static discharge. Recommended safety practices include keeping the work area clean‚ using proper PPE‚ and following lock‑out procedures during maintenance. A checklist verifies that all safety interlocks‚ emergency stops‚ and light curtains function correctly before the machine is returned to operation. These definitions and practices ensure operators and technicians maintain a safe environment while configuring and running CNC equipment. Additionally‚ the manual specifies that all safety interlocks must be tested during each maintenance cycle‚ and that any fault must be documented and corrected before the machine resumes operation. Ensures safety compliance‚.
Order Codes and Availability
For Mitsubishi Electric FA connection manuals‚ the official order codes are IB‑1501667 and IB‑1501668‚ which correspond to part numbers 100‑784 and 100‑785 respectively. These codes can be entered on the TIE Information Center or directly on the Mitsubishi support portal to request the latest PDF or printed edition. The manuals cover wiring diagrams‚ signal tables‚ configuration procedures‚ and safety definitions for the FA series. Availability is typically within 2–3 business days after order confirmation‚ with shipping options including standard ground and expedited air. Digital copies are provided immediately upon payment‚ while hard copies are dispatched from the nearest regional warehouse. For bulk orders or international shipping‚ contact the regional sales office to confirm lead times and customs requirements. All manuals are updated annually; the most recent revision is dated 2026‑05‑27‚ ensuring compatibility with the latest firmware releases. If a manual is out of stock‚ the support team offers a replacement or a digital download of the previous version. The order process requires a valid customer account and may include a small handling fee for overseas deliveries. Keep the order confirmation number for reference during installation or troubleshooting sessions. Delivery times depend on local logistics soon!.
Manual Access and Formats
Access to CNC connection manuals is streamlined through dedicated portals and direct ordering systems. For the Mitsubishi Electric FA series‚ the TIE Information Center accepts order codes IB‑1501667 and IB‑1501668 (part numbers 100‑784 and 100‑785). Upon confirmation‚ a PDF version is emailed instantly‚ while a printed copy is dispatched from the nearest regional warehouse. The PDF contains comprehensive wiring diagrams‚ signal tables‚ and configuration guidelines‚ and is available for download in both .pdf and .txt formats for compatibility with various software tools. The S625 CNC Interface and Connection Guide is offered as a free PDF download‚ with an optional text file for quick reference; users can view the document online without installation. For Fanuc manuals‚ the TIE portal provides a searchable database where operators can retrieve the latest connection guides in PDF format‚ ensuring they have the most up‑to‑date wiring and configuration instructions. All digital files are protected by a secure download link that expires after 48 hours to prevent unauthorized distribution. Users who prefer hard copies can request hard copies through the same ordering system‚ with shipping times ranging from 2 to 5 business days depending on location. The manuals also include a troubleshooting section that lists common error codes‚ diagnostic steps‚ and recommended corrective actions‚ helping operators quickly resolve issues and maintain optimal machine uptime. for all users. upkeep!